When the reading does not match the process
The clearest sensor fault symptom is a number that simply does not fit what is happening in the plant. A mould line can be cycling warmer than normal, a laser circuit may overheat, yet the display still sits at the setpoint. That mismatch is the first clue that the sensor, cable or input circuit needs attention.
In many South African plants, the fault is not a total failure. The probe may be drifting by 1 to 3 degrees, which is enough to upset tight temperature control on lasers and moulds. On process lines, that small error can change product quality, increase cycle time and make operators keep adjusting settings that are not the real problem.
- Display stays steady but the process temperature rises
- Setpoint changes have little or no effect
- One circuit behaves differently from the others
- Operators keep chasing the same warning without a clear cause
Signs the probe is drifting, not just reacting slowly
A slow response can point to a sensor that is dirty, loose or ageing. The reading may creep up or down long after the actual water temperature has changed. If the control panel takes too long to recover after a load change, the controller may be getting bad information, not bad cooling.
Drift often shows up after vibration, poor cable routing or repeated temperature cycling. In workshops around Alberton, Germiston and Boksburg, we often see probes affected by abrasion at the gland or by moisture in the terminal box. Coastal sites can have a different problem: humid air gets into connections and the signal starts to wander.
- Reading changes slowly after a tap, start-up or product change
- Temperature seems to overshoot and then settle late
- Alarm history shows repeated high and low deviations
- One sensor reads a few degrees off compared with a known reference
Common fault symptoms operators notice first
Operators usually spot the problem before the maintenance file does. The machine may trip without reason, cycle too often, or keep calling for cooling when the load is already stable. In some cases the controller hunts up and down because it is trying to correct a false reading.
It helps to watch for patterns rather than one-off events. A failed sensor can create false high temperature alarms, but a wiring fault may cause intermittent spikes only when the machine starts or when a cable moves. On chiller systems serving laser equipment, that can mean brief shutdowns that are hard to reproduce unless someone is logging the values properly.
- False high or low temperature alarms
- Short cycling of compressors or pumps
- Unstable control with repeated correction swings
- Trips that appear during vibration, start-up or load changes
Why a bad sensor can damage more than the sensor point
A faulty temperature input does not stay in one place. If the controller thinks the water is colder than it is, the system may undercool and push heat into the equipment. If it thinks the water is hotter than it is, the chiller may run longer than necessary, wasting power and putting extra strain on compressors, pumps and valves.
For mould cooling, that can mean uneven part finish and longer cycle times. For laser cooling, it can mean unstable performance and avoidable shutdowns. Process lines can suffer from inconsistent temperatures that are hard to trace back to the root cause because the problem looks like a cooling issue, not an instrumentation issue.
In South African plants dealing with load-shedding, backup starts and repeated restarts can make a weak sensor fail sooner. Each start-up adds vibration and heat cycling, so a probe that was already marginal can become unreliable very quickly.
What a proper fault check should include
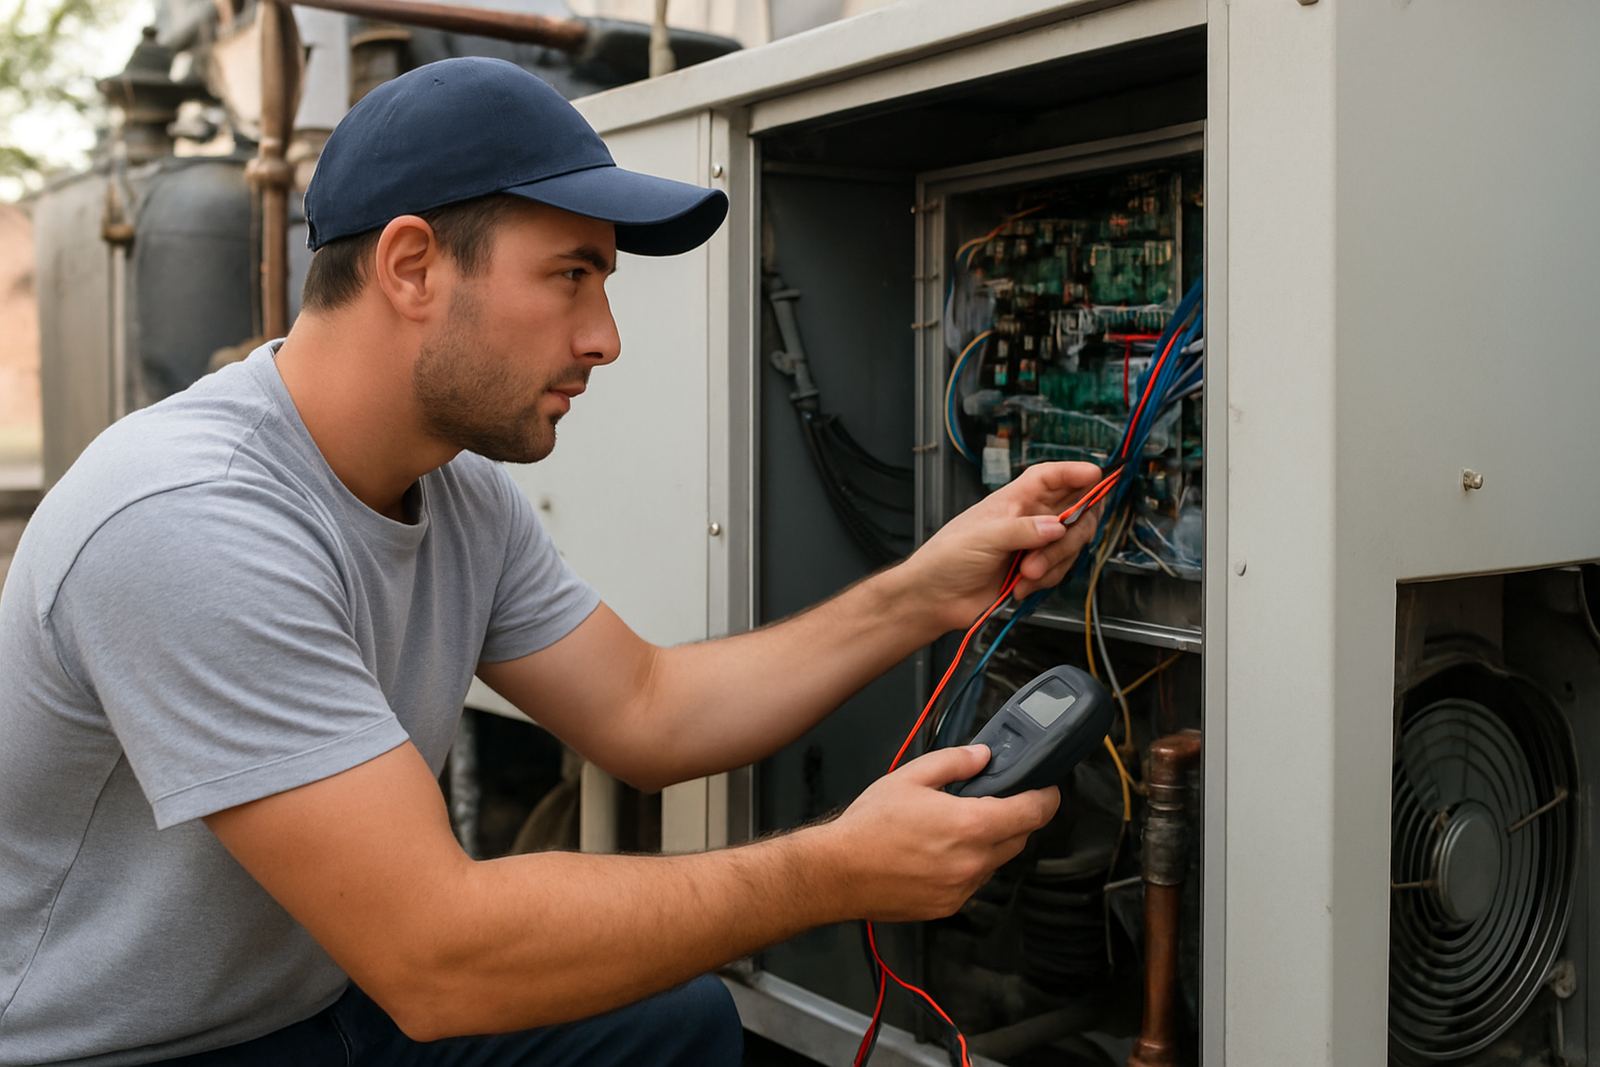
A quick visual check is useful, but it is rarely enough. The sensor should be compared against a known reference, the wiring inspected for looseness or corrosion, and the controller input checked for noise or broken screening. If the fault only appears under load, then the inspection must happen while the system is running, not only when it is idle.
At Raynen, our service teams look at the full cooling circuit, not just the probe. A sensor can be innocent while the real issue sits in a control panel, cable termination or water quality problem. That is why a proper fault check often includes commissioning data, pump performance and a look at how the unit behaves during a full cycle.
- Compare the reading with a calibrated reference
- Inspect cable glands, terminals and sensor mounting
- Check for moisture, corrosion or abrasion
- Review alarm history and operating patterns
A local example from a busy production site
A metal finishing plant serving the Ekurhuleni area called in because its chiller kept tripping on temperature alarm, mostly after lunch and during afternoon heat. The operator believed the load was changing, but the process conditions were steady. The fault turned out to be a drifting sensor on the return line, made worse by a loose connection in the panel.
Once the probe was replaced and the wiring secured, the control became stable again. The team also added a preventive maintenance check on sensor readings during routine service, which reduced nuisance trips and saved time during shift handovers. That sort of issue is common in high-use plants where the cooling system is expected to handle long hours and occasional power interruptions.
If your readings do not match the plant behaviour, treat it as a warning. A few minutes spent checking the sensor can prevent hours of lost production later.